Hey there, it’s Jake from [Your Furnace Tube Co.] – been fielding so many questions lately from folks across semiconductor manufacturing, heat treatment, and even solar panel production about furnace tube impurities. Like, last week I got a frantic call from a team at a mid-sized wafer fab, panicking because their QC lab flagged a tiny blip of iron in a batch of tubes they’d ordered, wondering if it’d mess up a $200k production run. That call stuck with me, because it’s exactly why I wanted to break down what actually counts as “acceptable” for these tubes – no stuffy textbook jargon, just real, on-the-ground knowledge from someone who’s been selling and troubleshooting these things for 12 years. Furnace Tube
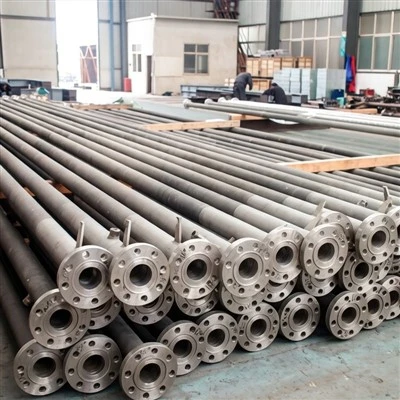
First off, let’s get one thing straight: furnace tubes aren’t one-size-fits-all. The acceptable impurity level isn’t a magic number I can rattle off without asking what you’re using the tube for. A quartz tube used in a high-temperature annealing furnace for semiconductors has way different standards than a stainless steel tube for melting aluminum, right? Semiconductor fabs work at temps up to 1200C+, where even a single stray atom of sodium or copper can ruin a wafer’s lithography layer – that’s a non-starter. But a tube for a metal heat treater might cut some slack on those trace metals if it’s still within specs for its intended use.
Let’s start with the core context that shapes all this: what impurities even matter here? I’m not talking about big chunks of rust or scratches (that’s a defect, not an impurity, and we’d never ship that anyway). Impurities are the trace elements in the tube material that can out-gas, leach, or diffuse into your load when it’s running. For the most common tube materials we work with – fused quartz (fused silica), 316L stainless steel, and high-purity alumina ceramic – the bad guys vary.
Take fused quartz first, since it’s our bestseller for semiconductor and R&D furnaces. Fused quartz is mostly SiO2, but when you make it, small amounts of other oxides sneak in: aluminum, potassium, sodium, iron, even titanium. The thing about quartz is that those alkali metals (sodium, potassium) are the real villains here. At temps above 800C, they can volatilize and condense on your wafers, causing micro-defects that kill yield. For semiconductor-grade quartz tubes, the standard is total alkali metal impurities (Na + K + Li) under 50 parts per billion (ppb) – that’s the threshold the Semiconductor Equipment and Materials International (SEMI) sets, and we don’t deviate from that. I’ve had a client push for 100ppb quartz tubes to save a few bucks, and let’s just say their next wafer run had a 30% yield loss from alkali contamination. No one wants that, especially when the price difference is like $200 for a 12-inch tube – not worth the risk.
Now, for non-semiconductor quartz use – say, glassblowing labs or small-scale metal annealing at under 700C? The bar is higher, like 500ppb total alkalis, and even a bit more iron is okay (up to 10ppm, vs 1ppm for semi-grade). At lower temps, those alkalis don’t volatilize enough to cause issues, so we can relax the spec a little to keep costs down for folks who don’t need the ultra-high purity.
Next up, 316L stainless steel tubes, which are super common for heat treating, food processing, and even some chemical furnaces. Stainless steel’s main impurities are carbon, sulfur, phosphorus, and trace metals like copper and lead. Wait, carbon is a big one here – 316L is “low carbon” for a reason. If carbon levels are too high (over 0.03%), when you run the tube at 1000C+, carbon can diffuse out and carburize your metal load, making it brittle or corroded. For heat treating of aerospace parts or medical implants, acceptable carbon is under 0.025% – that’s the medical-grade spec, and we hold our 316L tubes to that. For general metal annealing, like treating tool steel, we can go up to 0.03% with zero issues, because carburization isn’t a risk there.
Sulfur is another one in stainless – under 0.01% for most applications, but if you’re working with reactive metals like titanium, sulfur can cause hot cracking, so we drop that to 0.005% for those cases. Copper’s weird, too – some industries don’t care if there’s a little copper (under 0.2%), but if you’re using the tube for hydrogen annealing, copper can catalyze unwanted reactions, so we make sure those tubes have under 0.1% copper. I once had a oil and gas client ask for a stainless tube that could handle high pressure and corrosive gases – we had to test for chlorine and trace heavy metals, because even 0.001% of chlorine would cause pitting corrosion over time.
Then there’s alumina ceramic tubes, used for super-high temp work (1500C+). Alumina is Al2O3, but impurities like silica, magnesia, and iron oxide change its performance. For high-temperature furnaces that process ceramics or advanced semiconductors, we use 99.8% alumina, with silica under 0.1% and iron under 0.05%. At 1600C, even a tiny bit of silica will make the alumina soft, so that’s non-negotiable. If you’re just firing pottery, though, 95% alumina works fine, with impurities up to 5%, because you’re not pushing it to its melting point and contamination isn’t a big deal for pottery.
Wait, let’s talk about a common myth I hear all the time: “The fewer impurities, the better.” No, that’s not true. If you pay for semiconductor-grade quartz for a small lab that only runs at 500C, you’re wasting money. That ultra-high purity comes at a steep cost – we charge 2x more for semi-grade quartz than our general lab grade, because the manufacturing process requires extra purification steps (like zone refining) to knock those alkalis down. So the acceptable level is exactly what your process needs – no more, no less.
Another angle: how do impurities get measured, and why that matters for acceptability. We don’t guess at this. All our tubes go through ICP-OES (Inductively Coupled Plasma Optical Emission Spectroscopy) testing to measure trace elements, or GD-MS (Glow Discharge Mass Spectrometry) for ultra-high purity materials. For example, when we test a quartz tube for sodium, we don’t just eyeball it – we get a precise ppb number, and if it’s over the spec we quote you, it’s rejected. The only time we fudge a little is if a customer’s process is slightly variable – like, if their furnace runs at 750C instead of 800C, we can adjust the alkali spec to 75ppb, which cuts production time a bit and keeps their costs down. But we always confirm with their QC team first, no exceptions.
Let’s get real about real-world examples, because that’s what you care about. Last quarter, we had two orders for 10-inch quartz tubes. Order 1 was from a solar cell manufacturer, who needed tubes for diffusion processes at 900C. Their acceptable alkali level was 50ppb, so we shipped semi-grade, tested, and they used them with zero yield issues. Order 2 was from a hobbyist metal shop, needing tubes for annealing knife blades at 650C. Their acceptable alkali level was 500ppb, so we shipped our general-grade quartz, saved them $300 on the order, and they said the tubes worked perfectly. If we’d sent the semi-grade one to the hobbyist, they’d have complained it was too expensive, and they still would’ve gotten the same result.
What about edge cases? Like, if your tube has an impurity that’s not in the standard spec? Say you’re working with lithium-ion battery materials, and you’re worried about lithium contamination from the tube. We test for lithium specifically, and adjust the spec to under 10ppb – way lower than standard, because lithium is super reactive at high temps for battery processing. That’s the fun part of this job, actually – no two applications are the same, so we get to tweak specs to fit exactly what our customers need, instead of just selling a one-size-fits-all product.
Now, let’s talk about what happens if you go over the acceptable impurity level. For semiconductor clients? Yield loss, full stop. We had a client in Austin a couple years ago who ordered tubes from a cut-rate supplier that cut corners on purification, leading to 120 faulty wafers, a $150k loss, and a 6-month delay in their new product launch. They switched to us after that, because we’re transparent about our impurity levels and stand behind our testing. For metal heat treaters? Maybe a batch of parts that are brittle or corroded, which means rework or scrap. For ceramic firers? Discolored pottery or inconsistent hardness. It’s not worth the gamble to go over spec, even if the tube is cheaper.
Wait, but what if you go under spec? Is that a bad thing? Only if you’re overpaying. Like, if you’re a small lab doing R&D at 400C, paying for ultra-high purity quartz is like buying a sports car to drive to the grocery store – nice, but unnecessary. We always ask customers about their furnace temperature, what material they’re processing, and their required yield, then we match the impurity spec to that. No upselling, no hidden fees.
Let me wrap this up with the key takeaways, because I know you’re busy:
- Acceptable impurity levels aren’t universal – they’re tied directly to your tube material, operating temperature, and the sensitivity of your load.
- For fused quartz: total alkalis <50ppb for semi/ high-temp work, up to 500ppb for lower-temp general use; iron <1ppm for semi, up to 10ppm for general.
- For 316L stainless: carbon <0.025% for medical/aerospace, up to 0.03% for general; sulfur <0.005% for reactive metals, 0.01% for others.
- For alumina: 99.8% purity with <0.1% silica for >1200C work, 95% purity for lower-temp ceramic firings.
- Never pay for higher purity than you need – it’s just wasted money, and cutting corners on purity will cost you way more in lost product or time.
If you’re not sure what specs you need, just reach out. I don’t do sales pitches that don’t make sense for your process. Send us your furnace details, what you’re processing, and I’ll hook you up with a free impurity spec sheet and a quote tailored to your needs. No pressure, no fine print, just straight talk from someone who’s been in this game long enough to know that the last thing you need is a surprise impurity issue screwing up your work.
Talk soon,
Jake
Heating Furnace References:
SEMI Standard MF 1194-0708: Specification for Fused Silica for Semiconductor Processing Furnace Tubes
ASTM A262: Standard Practices for Detecting Susceptibility to Intergranular Attack in Austenitic Stainless Steels
Journal of the European Ceramic Society, Volume 41, 2021: Impurity Effects on High-Temperature Performance of Alumina Tubes for Industrial Furnaces
Jiangsu Dongfang Whole-Set Equipment Manufacturing Group Co., Ltd.
We are one of the most professional furnace tube manufacturers and suppliers in China, also support customized service. With abundant experience, we warmly welcome you to buy durable furnace tube from our factory. If you have any enquiry about pricelist, please feel free to email us.
Address: No. 9, Industrial Park, Xinqiao Town, Jingjiang City, Jiangsu Province
E-mail: dfctwm@163.com
WebSite: https://www.dongfangequip.com/
